ACD 2026: Let’s Connect

Great memories. Great connections. And even more to come!

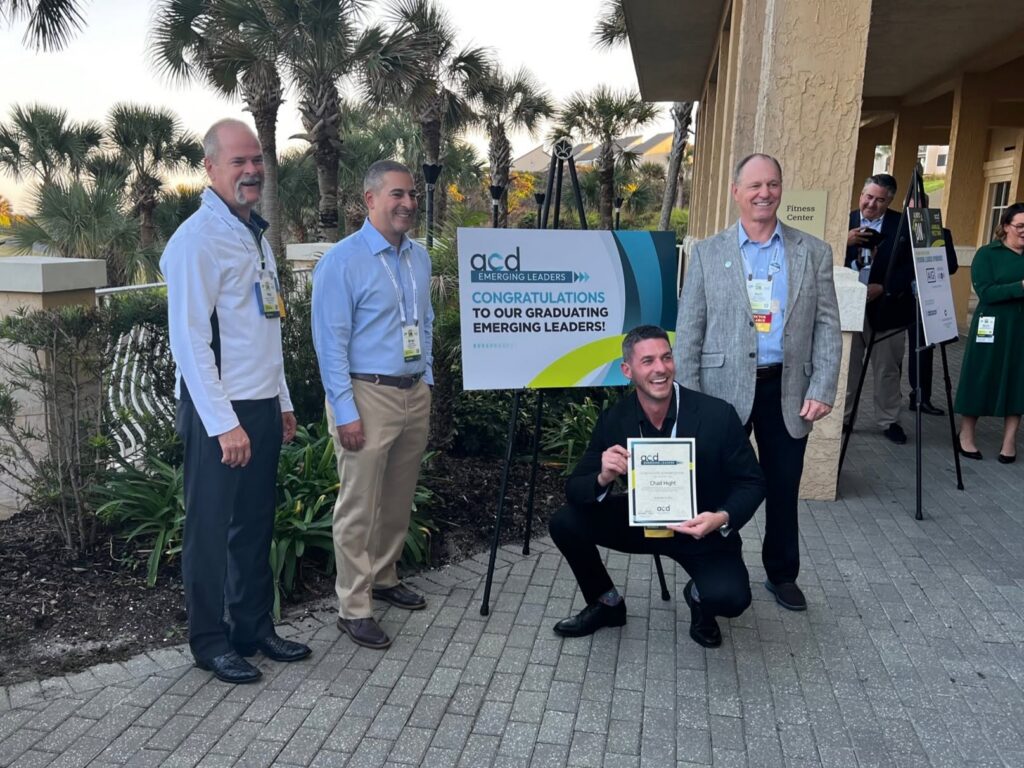
We’re less than a month away from the 2026 Alliance for Chemical Distribution (ACD) Annual Meeting.

As a returning sponsor, Brainerd Chemical is proud to support ACD and excited to reconnect with industry colleagues, exchange ideas, and help shape the future of chemical distribution.

Here’s to building on great relationships, creating new memories, and moving our industry forward together.

See you in Arizona!

Hydrogen Peroxide: The Spec Is Only the Starting Point

QA testing at Brainerd Chemical

Buying industrial hydrogen peroxide starts with concentration. Managing it well requires thinking beyond the spec sheet.

Industrial hydrogen peroxide buyers should evaluate more than concentration. A reliable H₂O₂ supply plan aligns the required concentration and grade with actual consumption, storage capacity, packaging, delivery frequency, handling requirements and contingency supply. Suppliers such as Brainerd Chemical can help connect those variables to the practical requirements of the operation.

Hydrogen peroxide looks straightforward on a purchase order: concentration, grade, quantity, delivery. Operationally, there’s more to it – a lot more.

The right H₂O₂ supply strategy connects chemistry, consumption, storage, handling and logistics. Get those aligned and peroxide can be remarkably straightforward. Get one wrong and procurement can create problems downstream.

Here are four things worth considering.

Start With the Process, Not the Percentage

Hydrogen peroxide is used across water and wastewater treatment, pulp and paper, food processing, chemical manufacturing and other industrial applications.

Each process puts different demands on the chemistry.

Brainerd supplies hydrogen peroxide in concentrations from 1% to 50%, with 34% and 50% representing significant industrial volumes.

But higher concentration isn’t inherently better. The right concentration is the one that fits the process, validated operating procedures, storage system and feed equipment while delivering the required chemistry efficiently.

Concentration Is Also a Logistics Decision

Concentration affects more than chemistry. It influences how much product must be transported, how frequently it needs to be delivered and how much inventory a facility can maintain.

A useful supply discussion therefore goes beyond ‘What concentration do you need?’ to also ask:

  • How much are you consuming?
  • How much can you safely store?
  • And how frequently do you want product arriving at the plant?

Those answers help determine whether drums, totes or bulk delivery make the most operational sense.

Plan for the Month That Isn’t Average

Average monthly consumption is useful for budgeting. Peak consumption is often more useful for supply planning.

A good H₂O₂ program accounts for production changes, seasonal demand, available storage, delivery lead times and minimum inventory levels.

If peroxide is critical to the process, there is another question worth answering before it becomes urgent: What’s Plan B?

Redundant hydrogen peroxide supply is key to consistent supply chain effectiveness. Do you have alternate sources and contingency plans established – before your primary supply chain is constrained.

Treat a Supply Change Like an Operating Change

A different concentration, package size or delivery method may look like a purchasing adjustment.

To the people operating the process, it may be much more.

Hydrogen peroxide is a strong oxidizer, and changes involving concentration, storage, transfer or handling should be reviewed against the applicable SDS, equipment requirements, established procedures and site EHS practices.

That’s where procurement, operations and technical expertise need to stay connected.

Make the Supply Plan Fit the Chemistry

Hydrogen peroxide purchasing doesn’t need to be complicated.

But it should be deliberate.

Start with the required chemistry. Match the concentration to the process. Build packaging and delivery around actual consumption and storage. Then, make sure there’s a credible plan for the days when demand—or supply—doesn’t behave as expected.

Brainerd Chemical supplies industrial hydrogen peroxide from 1% to 50%, including high-volume 34% and 50% concentrations, with packaged and bulk options supported by chemical distribution and transportation capabilities.

Need H₂O₂ pricing, availability or help evaluating a supply option? Talk with Brainerd Chemical.

Smarter Hydrochloric Acid Supply

Hydrochloric Acid order fulfillment safety checklist.

Concentration, packaging, delivery and supply reliability all matter when sourcing hydrochloric acid. Here are the questions industrial buyers should answer before placing an HCl order.

Hydrochloric acid, HCl, (also still commonly called muriatic acid) is a workhorse chemical used across water treatment, steel processing, chemical manufacturing, oil and gas and other industrial applications. But buying HCl isn’t simply a matter of finding a supplier with hydrochloric acid in inventory. Industrial buyers need the right concentration, grade and quantity—that is also in packaging their facility can receive—with a supply plan capable of keeping the process running.

Brainerd Chemical supplies hydrochloric acid in concentrations from 1% to 36%, including commonly requested 15%, 31% and 36% HCl, in packaged and bulk quantities.

Here are five things to consider when sourcing hydrochloric acid.

1. What HCl Concentration Do You Need?

Industrial hydrochloric acid is available in multiple concentrations, and the right choice depends on the application and process.

Common purchasing specifications include:

  • 15% hydrochloric acid
  • 31% hydrochloric acid
  • 31.5% HCl / 20° Baumé
  • 35–36% hydrochloric acid
  • Custom or diluted concentrations

Brainerd supplies HCl from 1% to 36%, providing flexibility for applications that require concentrated product as well as operations that prefer a ready-to-use dilution.

Don’t assume higher concentration is automatically better. The appropriate concentration should reflect your process requirements, storage and handling systems, feed equipment and established operating procedures.

2. Do You Need Bulk HCl, Totes or Drums?

How hydrochloric acid arrives at your facility matters almost as much as what’s in it.

A high-volume operation with appropriate storage may benefit from bulk hydrochloric acid delivery, while another facility may be better served by totes or drums.

Before requesting a quote, know:

  • Required concentration and grade
  • Typical order volume
  • Preferred package size
  • On-site storage capacity
  • Receiving and unloading requirements
  • Expected delivery frequency

Providing that information helps a supplier to recommend a practical combination of product, packaging and delivery.

It also prevents a common sourcing problem: finding the chemical you need but not in the form your facility can efficiently receive and use.

3. Where Is Your HCl Coming From?

Inventory is important. Reliable access to inventory is vital.

Hydrochloric acid is a high-volume industrial chemical, so transportation distance, distribution infrastructure and delivery capabilities can have a meaningful effect on supply reliability.

Ask potential suppliers:

  • Where will our HCl ship from?
  • What is the normal lead time?
  • What happens if that source becomes constrained?
  • Do you have alternate supply or distribution options?
  • Who manages transportation and delivery?

These questions become particularly important when HCl is critical to continuous operations.

A low price doesn’t provide much value if the product isn’t available when your tank reaches its reorder point.

4. Does the Supplier Understand Your Application?

A hydrochloric acid supplier should be able to do more than quote a concentration and price.

HCl is used for very different purposes across industry—from pH adjustment and ion-exchange regeneration to steel pickling, chemical processing and oilfield applications.

Those applications can have different requirements for concentration, purity, consumption, packaging and delivery.

Tell your supplier what the hydrochloric acid is doing in your process.

That conversation can uncover questions about product specifications, storage, delivery frequency or logistics before they become operational problems.

The goal isn’t simply to buy HCl. It’s to build an HCl supply program that fits the operation using it.

5. What Happens When Demand or Supply Changes?

Normal conditions don’t always reveal the strength of a chemical supply relationship.

Unexpected demand, transportation disruptions, maintenance outages and upstream supply constraints can quickly change availability.

That’s why buyers should understand a supplier’s contingency capabilities before they’re needed.

Ask:

  • Can you accommodate an unexpected increase in volume?
  • Are multiple concentrations or packaging options available?
  • Can you support changes in delivery frequency?
  • What communication can we expect during a supply disruption?
  • Are alternative supply options available?

These are particularly important questions for plants where an HCl shortage could slow or stop production.

Buying Hydrochloric Acid? Start With the Right Information.

When requesting a quote for industrial hydrochloric acid, provide your supplier with five basics: Concentration. Grade. Volume. Packaging. Delivery location. Then look beyond the quote. Consider where the product is coming from, how it will reach your facility and whether the supplier has the chemical expertise and logistics capabilities to support you when conditions change.

Brainerd Chemical supplies 1%–36% hydrochloric acid, including commonly used 15%, 31% and 36% concentrations, with packaged and bulk supply options supported by an experienced chemical distribution and transportation network.

Need hydrochloric acid pricing, availability or help determining the right supply option for your operation? Contact Brainerd Chemical.

7 Things to Look for in a Contract Chemical Manufacturer

The right contract manufacturer does more than blend your formula. Here’s how to evaluate the capabilities, controls and support that can affect everything from consistency thru delivery.

Finding a company with a tank and the ability to blend your product isn’t necessarily difficult. Finding one you want responsible for making it is a different matter. When you contract with another company to manufacture a chemical product, that company becomes an extension of your operation. Its equipment, people, quality systems, raw-material management, packaging capabilities and logistics can directly affect your ability to serve your own customers.

That makes the selection process about much more than available capacity or cost per gallon.

The better question is: Can this manufacturer consistently make what we need, safely handle the chemistry, adapt as our requirements change and reliably get the finished product where it needs to go?

Here are seven things worth examining before you make that decision.

1. Can They Handle Your Chemistry?

Start with the chemistry itself. A contract manufacturer may have plenty of blending capacity but limited experience with the materials your formulation requires. That distinction becomes especially important with hazardous, corrosive or otherwise difficult-to-handle chemicals.

Ask what products the manufacturer routinely handles—not simply what it is theoretically capable of processing. Does it have the appropriate equipment? Are operators trained for those materials? Are storage, transfer and containment systems appropriate for the chemistry? Does the facility have practical experience working with similar formulations?

This is an area where capabilities can differ substantially from one contract manufacturer to another.

At Brainerd Chemical, our blending operations handle both hazardous and non-hazardous materials. Our operators regularly work with difficult-to-handle chemicals including high concentrations of nitric acid and hydrofluoric acid, as well as hydrochloric acid, sulfuric acid, sodium hydroxide and other industrial chemistries.

The objective isn’t to find a company willing to take the job. It’s to find one with the experience and infrastructure appropriate for the job.

2. Does Their Capacity Fit Your Production Requirements?

A 10,000-gallon tank doesn’t necessarily mean a manufacturer is a good fit for a 500-gallon batch. And a facility optimized for small specialty batches may not be the right choice when demand grows substantially. That’s why it’s worth looking beyond total manufacturing capacity and asking about usable production flexibility.

Consider:

  • What are the practical minimum and maximum batch sizes?
  • Can the same manufacturer accommodate both routine and peak demand?
  • How much available capacity does it actually have?
  • Can production scale without changing manufacturers?
  • How does it schedule recurring versus intermittent production?

Brainerd operates more than 50 large-capacity tanks, with blending capabilities ranging from 55 to 40,000 gallons per batch. That range matters. A customer may initially need relatively modest production quantities, then require substantially more as a product gains customers or enters additional markets. The ability to accommodate that growth can eliminate the disruption of qualifying another manufacturer later.

3. How Do They Protect Product Consistency?

Capacity gets attention. Consistency keeps customers. When another company manufactures your product, you need confidence that batch 20 will meet the same requirements as batch one. That means understanding the manufacturer’s process controls before production begins.

Ask how raw materials are managed, how formulations and production instructions are controlled, what quality checks are performed and how finished product is documented.

Equally important: What happens when something doesn’t go according to plan?

A good evaluation should explore how the manufacturer handles deviations, off-specification material, documentation and corrective actions. For established formulations, contract or toll manufacturing should allow the customer to retain ownership of the formula while the manufacturing partner assumes responsibility for producing the product to the agreed requirements. Brainerd supports toll manufacturing as well as custom formulation within its blending operation. Your formula may be proprietary. Your expectations for how it is manufactured shouldn’t be mysterious.

4. Can They Handle What Happens After the Blend?

A finished blend isn’t necessarily a finished product. It may still need to be transferred, packaged, labeled, stored and shipped. If each step requires another vendor, the apparent simplicity of contract manufacturing can quickly become a complicated supply chain.

Suppose one company blends your product, another packages it, a warehouse stores it and a third-party carrier transports it. You now have multiple handoffs, schedules and points of accountability to manage. That’s why it pays to ask a prospective manufacturer what happens after the blending tank.

Brainerd integrates chemical blending with packaging, storage, distribution and transportation. Depending on the product and application, those capabilities can include drums, totes, bulk tanker quantities, custom packaging, white-label programs and drop shipping.

That can turn several individual transactions into one coordinated process. For your customer, fewer handoffs can mean fewer opportunities for something to get lost between them.

5. Who Is Responsible for Transportation?

Transportation is easy to treat as the final step in manufacturing. For chemicals, it should be part of the manufacturing conversation from the beginning. Ask whether the contract manufacturer manages transportation directly or hands finished product to a third-party carrier. Find out who coordinates scheduling, what experience drivers have with the products being transported and who is accountable when a delivery problem occurs.

This becomes particularly important with hazardous or difficult-to-handle materials.

Brainerd operates company-owned trucks with drivers trained in chemical handling and off-loading. Transportation is part of our broader service model rather than an unrelated transaction at the end of production. That kind of integration can matter when timing, handling and communication are just as important as getting the chemistry right.

6. Can They Adapt When Your Requirements Change?

The product you manufacture today may not be the product you need three years from now. Volumes change. Customers request different package sizes. Formulations evolve. New markets create different specifications. Seasonal demand can create production spikes.

Before selecting a contract manufacturer, ask what happens when the program changes.

Can the manufacturer accommodate a different batch size? Add packaging options? Help adjust a formulation? Store finished inventory? Support a new delivery model? A real-world example comes from Brainerd’s 2024 manufacturing agreement with Bioeutectics, a biotechnology company developing bio-based industrial solvents. The relationship paired an emerging chemistry company with Brainerd’s established manufacturing capabilities.

For Brainerd COO Neil Morgan, the partnership represented something larger than simply filling available production capacity: “We’re proud of this partnership and our opportunity to lead change from within the chemical industry by championing more innovative and environmentally responsible chemical solutions that our customers want.”

That’s an important distinction. A capable contract manufacturer shouldn’t limit what comes next. Ideally, it should help make what’s next possible.

7. Are You Buying Tank Time—or Gaining a Chemical Partner?

Eventually, most contract manufacturers can tell you about their tanks, equipment and throughput.

Those things matter.

But when a supply problem develops, a formulation changes, demand suddenly increases or a difficult technical question arises, you’re probably not going to call the tank. You’re going to call the people behind it. That’s why technical expertise, communication and problem-solving ability belong on the evaluation list alongside price and production capacity.

At Brainerd, we see that as part of the job. As Neil Morgan recently explained: “Our customers expect more than dependable chemical supply. They value technical expertise, operational insight and the ability to help solve tomorrow’s challenges—not just fill today’s orders.”

That philosophy is particularly relevant to contract manufacturing. When another company is responsible for making your product, you’re trusting it with more than a purchase order. You’re making its people, processes and capabilities part of your own supply chain.

Look Beyond the Blend

Choosing a contract chemical manufacturer shouldn’t come down to one question about price or capacity. Look at the complete operation.

  • Can they handle the chemistry?
  • Can they produce it consistently at the volumes you need?
  • Can they package and store it appropriately?
  • Can they manage transportation?
  • Can they adapt when your requirements change?

And perhaps most importantly: When something unexpected happens, do you have confidence in the people answering the phone?

Brainerd Chemical brings together custom and contract blending, difficult-to-handle chemical expertise, flexible batch capabilities, packaging, warehousing and company-operated transportation within one chemical supply network.

Because the best contract manufacturer shouldn’t simply be able to make your product.

What Food Processors Should Know About Peracetic Acid (PAA)

As food safety standards tighten and sustainability expectations rise, peracetic acid (PAA) is becoming the sanitizer of choice for processors seeking reliable microbial control, operational efficiency, and environmental stewardship.

What disinfectant should food processors use? There is no universal ‘best’ disinfectant for every food processing operation, but peracetic acid (PAA) has become one of the fastest-growing sanitation technologies because it provides rapid, broad-spectrum antimicrobial performance while supporting water conservation, sustainability initiatives and operational efficiency. Many processors now evaluate PAA based on its total operational value rather than cost per gallon alone.

Why More Food Processors Are Switching to PAA

Food processors are not abandoning chlorine overnight—but many are asking a different question: ‘Which sanitizer delivers the best overall operational value?’ Modern sanitation programs are increasingly evaluated by food safety, production uptime, water use, wastewater management, worker safety, sustainability, and total operating cost. That’s where PAA continues to gain momentum.

Why PAA Stands Out

Peracetic acid has become increasingly popular because it checks multiple boxes at once. It offers rapid antimicrobial performance, broad-spectrum effectiveness, strong performance in the presence of organic matter, minimal environmentally persistent byproducts, support for water conservation initiatives and compatibility with modern sustainability programs. Rather than solving a single sanitation challenge, PAA often improves several parts of an operation at once.

“Food processors aren’t simply replacing one sanitizer with another—they’re rethinking how sanitation supports the entire operation. The conversation today includes food safety, water stewardship, operational reliability, and long-term sustainability. Peracetic acid has become an important tool because it helps facilities address all of those objectives simultaneously.”

— Derk Pinkerton, Market Manager – Water Treatment, Brainerd Chemical Company

Today, PAA is commonly used across broad food processing applications:

  • Poultry, beef, pork and seafood processing
  • Fresh produce washing
  • Dairy and beverage production
  • Breweries and wineries
  • Process water treatment
  • Food-contact surface sanitation
  • Select Clean-in-Place (CIP) applications

The Cheapest Sanitizer Can Become Your Most Expensive Decision

Chemical price is only one line on the budget. Production interruptions, equipment downtime, wastewater treatment, worker training and environmental reporting all influence the true cost of a sanitation program. Leading processors increasingly evaluate total operational value rather than cost per gallon.
The question is no longer whether to evaluate PAA—but where it can create measurable value in your operation. Peracetic acid isn’t intended to replace every traditional sanitizer, but its growing adoption reflects a broader shift toward smarter sanitation strategies.
Whether you’re expanding production, improving food safety protocols, reducing wastewater challenges or exploring more cost-effective solutions, Brainerd Chemical’s water treatment specialists can help evaluate where peracetic acid fits into your operation.

Brainred’s team works alongside food processors to develop practical, application-specific sanitation programs backed by technical expertise, dependable supply, and decades of experience serving North American industry. Contact Brainerd Chemical today to schedule a consultation with a member of the water treatment team and discover whether PAA is the right solution for your facility.

Five Questions Every Chemical Procurement Team Should Ask

Price is only one part of the equation. Today’s leading manufacturers evaluate chemical suppliers based on reliability, expertise, safety, and long-term partnership potential.

Two suppliers submit bids for the same chemical. One is 4% less expensive. The other has a stronger safety record, regional inventory, technical support, and decades of regulatory expertise.
Which supplier represents the better business decision? For experienced procurement leaders, the answer is becoming increasingly clear: the lowest price rarely delivers the lowest total cost.

So, What Should You Expect (Demand) From Your Chemical Supplier?

The best chemical suppliers offer more than competitive pricing. Manufacturers should evaluate supply reliability, technical expertise, regulatory support, safety performance, inventory capabilities, packaging flexibility, logistics, and long-term partnership potential. Choosing the right supplier can reduce operational risk while improving production continuity and total cost of ownership.

  1. Can They Deliver Consistently?
    Your production line can’t wait for a delayed shipment. Reliable delivery protects production schedules—and customer commitments. Evaluate:
    • JIT capabilities
    • Inventory availability
    • Multiple distribution locations
    • Emergency response capabilities
    • Proven delivery performance
    • Supply chain resilience
  2. Do They Bring Technical Expertise?
    Industrial chemicals are rarely “plug-and-play.” Technical guidance often creates more long-term value than incremental price savings. True partners help you optimize your supply chain:
    • Product selection
    • Handling procedures
    • Storage requirements
    • Application performance
    • Regulatory compliance

The strongest customer relationships begin long before the first shipment arrives. Our role is to help customers reduce operational risk by combining dependable supply with practical technical expertise that supports their long-term success.
— Brian Miller, President, Brainerd Chemical Company

  1. Is Safety Part of Their Culture?
    Strong safety cultures often translate into stronger operational performance. Safety shouldn’t end when a shipment leaves the loading dock. Look for suppliers with demonstrated commitment to:
    • Employee training
    • Regulatory compliance
    • Product stewardship
    • Responsible transportation
    • Emergency preparedness
  2. Can They Grow With Your Business?
    Scalable partnerships reduce the need to change suppliers as operations evolve. Today’s supplier should also support tomorrow’s production goals. Ask about:
    • Packaging options
    • Technical resources
    • Regional inventory
    • Manufacturing capabilities
    • Capacity for future growth
  3. Will They Be a Partner—or Just a Vendor?
    The best suppliers solve problems before they become disruptions. They proactively communicate, share technical knowledge, and collaborate to improve operations—not simply process purchase orders.
    Those relationships often create measurable value long after the initial contract is signed.

Stewardship – Value Beyond Price

Procurement has evolved. Today’s purchasing decisions influence production reliability, operational efficiency, sustainability initiatives, regulatory confidence, and long-term business resilience.
The organizations creating the greatest competitive advantage are not simply buying chemicals – they are choosing strategic partners.
The right chemical supplier does far more than deliver product. They help manufacturers reduce risk, improve operational performance, and prepare for future growth.
As supply chains become more complex and customer expectations continue to rise, procurement decisions have never carried greater strategic importance.
The question is no longer: “Who offers the lowest price?”
The question is: “Who will help us operate more successfully over the next decade?”

Move Toward Success

Whether you’re evaluating a new supplier, expanding production, or strengthening supply chain resilience, Brainerd Chemical’s technical and logistics specialists work alongside manufacturers to build dependable, long-term partnerships that support operational success.
Contact Brainerd Chemical to learn how the right supplier relationship can create value well beyond the purchase order.

The New Competition for Chemicals

How America’s manufacturing resurgence is changing the way chemical buyers think about supply chain resilience.

If you’ve been following industrial development across the United States, you’ve likely noticed the pace of expansion accelerating.

New semiconductor facilities. Battery plants. Data centers. Advanced manufacturing campuses.

Across the country, major investments in domestic manufacturing are increasing demand for the chemicals that keep modern industry running.

Hydrofluoric acid. Nitric acid. Sulfuric acid. Sodium hydroxide. Water treatment chemistries. Specialty process chemicals.

Demand is growing across the board. For chemical buyers and operations leaders, the question isn’t whether demand is increasing—it’s whether supply chains are prepared to keep pace.

What does manufacturing expansion mean for chemical supply chains? Supply chain resilience is the ability to maintain reliable access to critical materials despite fluctuations in demand, transportation disruptions, market volatility, or supplier constraints. For chemical buyers, that means dependable supply, flexible packaging options, reliable logistics networks, and suppliers capable of supporting long-term growth.

New Facilities, New Demand

The semiconductor industry is one of the most visible examples. As new fabrication facilities come online across the United States, demand is increasing for the chemicals used to clean wafers, etch circuits, treat water, manage waste streams, and support production processes.

In many cases, these industries aren’t competing for the exact same chemical products—but they are competing for the same manufacturing capacity, transportation resources, packaging assets, and distribution networks. Many similar chemistries are used by:

  • Water treatment facilities
  • Industrial manufacturers
  • Agricultural operations
  • Energy producers
  • Metal processors

That’s why semiconductor growth matters to far more than semiconductor manufacturers.

The Questions Buyers Are Asking

Most procurement and operations teams have experienced some form of supply chain disruption over the past several years.

Extended lead times.

Transportation delays.

Packaging shortages.

Unexpected demand spikes.

The result is often the same: A delayed railcar. A missed delivery window. A production schedule that suddenly needs to be adjusted. Small disruptions can create outsized consequences when critical materials aren’t available when they’re needed.

As demand grows, these are the conversations happening in procurement offices and operations meetings across the country:

  • Can our supplier support future growth?
  • Do they have packaging flexibility?
  • How resilient is their logistics network?
  • Do they have multiple sourcing options?
  • Can they maintain supply during periods of increased demand?

Those questions are increasingly important as domestic manufacturing capacity continues to expand.

Reliability Is Becoming a Competitive Advantage

Price will always matter. But if you’ve ever had a critical shipment delayed, you know the real cost of supply disruption often extends far beyond the purchase order.

A delayed shipment, unexpected shortage, or disruption in supply can quickly affect production schedules, inventory planning, customer commitments, and operating costs. That’s why manufacturers are placing greater emphasis on supplier capabilities, geographic reach, inventory strategies, packaging options, and transportation expertise.

In an environment where demand is growing, reliability becomes a competitive advantage.

Looking Ahead

America’s manufacturing resurgence is creating exciting opportunities across multiple industries. It is also reshaping chemical supply chains.

Organizations that understand how these changes affect sourcing, inventory planning, logistics, and supplier relationships will be better positioned to navigate future demand and support long-term growth. For chemical buyers, the conversation is becoming less about securing the lowest price and more about securing dependable access to the materials that keep operations moving.

As domestic manufacturing continues to grow, the organizations that invest in resilient supply chains today will be better positioned to respond to future demand, manage disruption, and maintain a competitive advantage. 

About Brainerd Chemical Company

Brainerd Chemical Company is a leading North American manufacturer, distributor, packager, and logistics provider of specialty and commodity chemicals. Through chemical manufacturing, custom packaging, private-label programs, contract packaging, and supply chain support, Brainerd helps customers operate safely, maintain compliance, and keep critical operations moving.

Media Inquiries

Brainerd Chemical Company

📞 +1 (918) 622-1214

🌐 www.BrainerdChemical.com

Safety Happens Between People, Not Policies 

Why the Strongest Safety Programs Depend on People, Not Policies. 

Every chemical facility has procedures. Training is scheduled. Audits are completed. Safety meetings fill calendars. 

Yet the safest organizations know something that can’t be captured in a binder or measured on an inspection form: safety is ultimately a people business. 

Long before an incident occurs—or is prevented—employees make hundreds of decisions that influence outcomes. They ask questions. Double-check a connection. Pause a task that doesn’t feel right. Speak up when they see a potential risk. 

Those moments are where safety culture is built. Yet the organizations that consistently achieve the best safety outcomes understand an important truth: Safety is not created during an audit. It is created every day through a culture fostered by leadership and embraced by people. 

Policies, procedures, and regulations establish an essential foundation. They define expectations and provide structure. But real safety performance is determined by thousands of decisions made by employees, supervisors, operators, drivers, and leaders throughout the course of normal operations. 

The strongest safety cultures emerge when safety becomes more than a requirement. It becomes a shared responsibility. 

Safety culture in chemical manufacturing is built through daily behaviors, decisions, and conversations—not just audits, training programs, or compliance requirements. While policies and procedures provide the foundation, lasting safety performance depends on leadership, communication, teamwork, and employee engagement. Organizations with strong safety cultures create environments where every employee takes ownership of safety, identifies risks, and actively looks out for one another. 

Why Compliance Alone Doesn’t Create a Safety Culture 

In highly regulated industries such as chemical manufacturing and distribution, compliance matters. Regulatory standards exist for good reason. They help establish consistent practices designed to protect employees, communities, customers, and the environment. 

But compliance alone does not create a safety culture. 

Organizations can maintain complete documentation, conduct required training, and still struggle to create an environment where employees feel empowered to identify risks, stop unsafe activities, or speak up when something doesn’t seem right. 

The difference lies in engagement. 

When employees view safety as a management responsibility, opportunities can be missed. When employees view safety as everyone’s responsibility, awareness becomes part of daily operations. 

Every Employee Influences Safety 

One of the most powerful characteristics of a mature safety culture is the understanding that every individual contributes to safer outcomes. 

A driver completing a pre-trip inspection. 

A production employee identifying a potential hazard. 

A supervisor reinforcing a best practice. 

A team member asking a question before proceeding with an unfamiliar task. 

These moments may seem small, but collectively they shape workplace culture. Mike Hodnett, General Branch Manager of Brainerd’s Dunn facility, reminds us that every single employee plays a role in creating a workplace built on thoughtful decisions and shared responsibility. Organizations with strong safety records understand that responsibility cannot rest solely with management, policies or safety notices. It must be a culture embraced by the entire workforce. 

Leadership Sets the Tone 

While safety belongs to everyone, leadership plays a critical role in establishing expectations and reinforcing behaviors. 

Employees pay close attention to what leaders prioritize. When production schedules consistently outweigh safety concerns, employees notice. When leaders invest in training, encourage communication, and actively participate in safety discussions, employees notice that too. 

At Brainerd Chemical, COO Neil Morgan often emphasizes that effective safety programs must be practical enough to work in the real world. As he recently explained, successful safety cultures are built by creating processes that are “clear, practical and actionable” and supporting them through strong communication and teamwork. 

That philosophy reflects an important reality: safety procedures only create value when people understand them, trust them, and consistently apply them. 

The Connection Between Teamwork and Safety 

Safety is often discussed as an individual responsibility, but it is equally a team effort. 

Communication, trust, and accountability are critical components of effective safety performance. 

Teams that communicate openly are more likely to identify hazards before they become incidents. 

Teams that trust one another are more willing to ask questions and raise concerns. 

Teams that hold one another accountable create environments where safe behaviors become standard operating practice rather than occasional reminders. 

In many ways, safety serves as a reflection of organizational teamwork. Strong teams tend to operate more safely because they actively look out for one another. 

Building a Better Industry 

In chemical manufacturing, safety culture is not defined by the absence of incidents. It is defined by the daily behaviors, decisions, and conversations that help prevent them. 

Creating a stronger industry requires more than regulatory compliance. It requires leadership, accountability, continuous improvement, and a shared commitment to doing the right thing—even when no one is watching. 

That commitment is reflected in the perspectives shared throughout Brainerd’s organization: practical safety processes, clear communication, strong teamwork, thoughtful decisions, and shared responsibility. Together, these principles help create an environment where safety is not simply a program—it becomes part of how people work every day. 

The organizations that will lead the future of the chemical industry are not simply those with the strongest products or largest facilities. They will be the organizations that create cultures where safety is embedded in every decision, every conversation, and every action. 

Because the strongest safety programs are not built during audits. They are built between them. 

About Brainerd Chemical Company 

Brainerd Chemical Company helps manufacturers, municipalities, agricultural operations, and industrial organizations solve complex chemical challenges safely and reliably. As a leading U.S. chemical manufacturer and distributor, Brainerd combines quality products, technical expertise, and responsive service to help customers succeed every day. 

Media Inquiries 

Brainerd Chemical Company 

📞 +1 (918) 622-1214 

🌐 www.BrainerdChemical.com 

Smarter Chemical Packaging

Learn how the right packaging solutions can help you improve safety, compliance, and operational performance.

A chemical package has one job: arrive safely and perform exactly as expected.

Yet packaging decisions influence far more than transportation.

The right packaging strategy can improve safety, simplify compliance, reduce handling costs, support private-label programs, and strengthen supply chain performance. The wrong one can create operational headaches long after the shipment leaves the facility.

Proven chemical packaging providers like Brainerd Chemical Company help manufacturers improve safety, compliance, operational efficiency, and supply chain reliability.

What are chemical packaging services?
Chemical packaging services help manufacturers safely package, label, store, transport, and distribute chemical products. Services may include custom packaging, private labeling, contract packaging, bulk handling, regulatory compliance support, and logistics coordination. Many manufacturers also rely on chemical packaging providers to support brand expansion, new product launches, and regional distribution strategies.

Packaging Impacts More Than Transportation

Every chemical operation is different. What works well for one facility may create challenges for yours. Container size, material compatibility, handling requirements, storage constraints, transportation methods, and end-user needs all influence the right packaging strategy.

When packaging is treated as an afterthought, organizations often experience:

  • Increased handling and labor costs
  • Product waste and container damage
  • Storage inefficiencies
  • Transportation limitations
  • Higher regulatory risk
  • Greater potential for spills and exposure incidents

These costs rarely appear on an invoice, but they can significantly impact operations over time.

Safety Starts With the Right Container

For hazardous and specialty chemicals, packaging is a critical part of risk management.

The right packaging helps protect employees during handling, transportation, storage, and use. The wrong packaging can increase exposure risks, create unnecessary handling steps, and complicate emergency response efforts.

Your packaging strategy should support safe operations from the moment a product is filled until it reaches its final application.

That requires more than selecting a container. It requires understanding how the product will move through the entire supply chain.

Packaging That Scales With Demand

Many organizations face changing production schedules, fluctuating demand, and evolving customer requirements. A packaging partner should be able to support a variety of formats, including pails, drums, totes, bulk shipments, and customized white-label packaging solutions.

Flexibility helps organizations adapt to changing business needs without disrupting operations or introducing unnecessary risk.

Packaging That Supports Your Brand

Chemical packaging involves more than filling containers. It requires an understanding of chemical compatibility, labeling requirements, transportation regulations, quality control procedures, and customer-specific specifications.

Packaging experience matters because many problems can be prevented long before a shipment leaves the facility.

Private labeling and white-label chemical packaging allow your organization to bring products to market under your own brand while relying on an experienced packaging partner to execute behind the scenes. You’ll better maintain consistency across packaging formats, support regulatory compliance, and simplify supply chain management without requiring additional internal resources.

Whether you need branded containers, custom labeling, blind shipping, or specialized packaging requirements, flexibility matters because it supports both operational goals and business growth.

This is especially valuable when your organization is looking to expand product offerings, enter new markets, or streamline distribution without investing in additional packaging infrastructure.

Brainerd Chemical Company supports a wide range of packaging requirements, including custom packaging, contract packaging, private-label programs, blind shipping, and bulk packaging solutions. Packaging operations support everything from pails and drums to totes and bulk shipments, including products that require specialized handling due to corrosive, oxidizing, or hazardous characteristics.

With packaging operations strategically located across the United States, Brainerd helps customers maintain supply chain flexibility while supporting regional and national distribution requirements.

Packaging Is a Strategic Decision

Whether packaging nitric acid, sulfuric acid, hydrochloric acid, sodium hydroxide, or specialty chemical formulations, the requirements extend far beyond selecting a container. When evaluating packaging options, you’ll need to consider material compatibility, transportation regulations, storage conditions, customer requirements, and worker safety.

The best packaging programs do more than move products from one location to another. They help protect your employees, support compliance, strengthen customer relationships, and create operational flexibility.

Whether the need is bulk transportation, custom packaging, private labeling, or specialized handling for hazardous chemicals, the right packaging partner becomes an extension of your operation.

That’s why the most effective organizations no longer view packaging as a shipping function. They view it as a competitive advantage.

About Brainerd Chemical Company

Brainerd Chemical Company is a leading North American manufacturer, distributor, packager, and logistics provider of specialty and commodity chemicals. Through chemical manufacturing, custom packaging, private-label programs, contract packaging, and supply chain support, Brainerd helps customers operate safely, maintain compliance, and meet the demands of an increasingly complex marketplace.

Media Inquiries

Brainerd Chemical Company

📞 +1 (918) 622-1214

🌐 www.BrainerdChemical.com

The AI Boom Has a Water Treatment Problem

Data centers are becoming one of America’s largest water treatment challenges – Brainered Chemical has the solution.


Artificial intelligence is fueling a massive wave of data center construction across the United States. Most people focus on the servers, chips, and electricity required to power AI. Few realize another resource is becoming just as critical: Water.

Data centers generate enormous amounts of heat. Keeping those systems cool requires significant water resources—and effective water treatment.

According to research from Uptime Institute, water management has become a strategic consideration for data center operators, with cooling system design playing a central role in determining water consumption, sustainability performance, and long-term operational resilience.

As AI workloads continue to increase cooling demands, operators are under growing pressure to reduce water use while maintaining reliability.

Here are six reasons water is becoming one of the biggest challenges facing modern data centers.

1. AI Is Driving Water Demand

More computing power creates more heat. More heat requires more cooling. More cooling often requires more water.

As AI adoption accelerates, data centers are consuming millions of gallons annually to support operations.

2. Water Quality Impacts Reliability

Cooling systems depend on clean, properly treated water. Without effective treatment, operators can face:

  • Scale buildup
  • Corrosion
  • Reduced efficiency
  • Increased maintenance
  • Unplanned downtime

Reliability starts with a strategic approach to sustainable water quality.

3. Sustainability Goals Are Raising Expectations

Leading data center operators are under increasing pressure to reduce both energy and water consumption. That is driving investment in:

  • Water reuse
  • Cooling optimization
  • Efficiency improvements
  • Advanced treatment technologies

4. Every Gallon Counts

Many new facilities are being built in fast-growing regions where water resources are already under pressure. Communities, regulators, and investors are paying closer attention to how water is managed.

Water treatment is no longer just a maintenance function. It has become a strategic asset and a critical factor in:

  • Operational reliability
  • Sustainability performance
  • Infrastructure planning
  • Risk management

As data centers expand, operators are investing in smarter monitoring, automation, chemistry optimization, and water conservation strategies.

The goal is simple: Use less water while maintaining maximum reliability.

5. Smarter Water Treatment Can Reduce Cost, Risk, and Environmental Impact

As data center operators look for ways to improve efficiency and sustainability, many are reevaluating traditional water treatment programs.

One area receiving increased attention is the use of advanced oxidizing chemistries such as peracetic acid (PAA) for microbiological control in industrial water systems.

Compared to some conventional treatment approaches, PAA-based programs can help facilities:

  • Improve control of biological growth
  • Reduce system fouling and performance losses
  • Support water reuse and conservation initiatives
  • Minimize residual environmental impact
  • Simplify handling and operational requirements
  • Lower total treatment costs in certain applications

For operators focused on uptime, sustainability, and operational efficiency, the right water treatment strategy can create benefits that extend far beyond water quality alone.

The conversation around data center cooling is increasingly becoming a conversation about water efficiency and sustainability. Operators are looking for solutions that help protect critical assets while reducing complexity, lowering environmental impact, and making better use of water resources. That’s where innovative chemistries like peracetic acid can play an important role.

Why This Matters

The future of AI depends on data centers. The future of data centers depends on cooling. And cooling depends on water.

As operators face growing pressure to improve reliability, reduce environmental impact, and optimize operating costs, water treatment is becoming a strategic advantage rather than simply a maintenance function.

One solution receiving increased attention is peracetic acid (PAA). Data centers depend on efficient cooling systems to maintain uptime and protect critical computing infrastructure. PAA can help control microbiological growth in cooling water systems, reducing the potential for biofouling that may impair heat transfer and system performance. As operators pursue reliability, sustainability, and water stewardship goals, PAA is increasingly being evaluated as part of modern industrial water treatment programs.

“Reliable cooling doesn’t happen by accident. It starts with water. As data centers grow larger and more powerful, operators are looking for ways to improve efficiency, reduce water consumption, and protect critical infrastructure. That’s creating new opportunities for smarter water treatment.”

Derk Pinkerton, Market Manager – Water Treatment, Brainerd Chemical Company

At Brainerd Chemical, we help industrial and water treatment customers evaluate solutions that support cooling system performance, improve operational efficiency, and align with evolving sustainability objectives.

Because when it comes to supporting the infrastructure behind AI, every gallon—and every decision—matters.

About Brainerd Chemical Company

Brainerd Chemical Company is a leading U.S. manufacturer and distributor of specialty and commodity chemicals, committed to safely delivering the solutions customers need, the expertise they value, and the reliability they depend on — every day.

Media Inquiries

Brainerd Chemical Company

📞 +1 (918) 622-1214

🌐 www.BrainerdChemical.com